If you’ve ever stood on a molding factory floor at 2 a.m., watching a team of technicians huddle around a Molding Main Unit (MMU) that’s currently churning out a batch of plastic automotive interior trim, you already know this: the mold changing process isn’t just a task—it’s a make-or-break link between an order that’s running late and one that arrives on spec, on time, and ready to ship. As a third-generation MMU supplier, I’ve spent 18 years talking to molding plant managers who lose hundreds of thousands of dollars in downtime every year because their mold change process is broken, rushed, or left to whatever part-time intern can spare an hour. Today, I’m pulling back the curtain on how our customers do it right—and what our MMUs bring to the table to make that process faster, safer, and less error-prone. Molding Main Unit
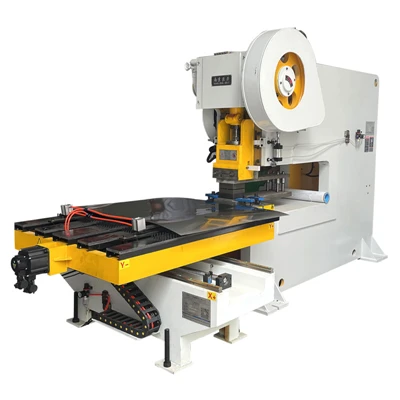
Let’s start with a quick reality check: mold changing on a standard injection molding machine isn’t the same as on an MMU. A conventional machine might hoist a single mold in and out of its platens every 2 to 4 hours, a process that requires disconnecting cooling lines, electrical sensors, and ejector pin connections by hand, all while the machine sits idle. An MMU is purpose-built to hold two (or sometimes three) separate molds, mounted on a rotating or sliding carriage that shuttles one into the molding cavity while the other sits prepped and waiting outside. That’s the core difference—and it’s why mold changing on an MMU should take less than 10 minutes, not 45. But it doesn’t happen by accident. It’s a structured, 5-step process that we engineer into every MMU we build, and that we train our customers to master long before they ever need to swap molds mid-run.
Step one: pre-change preparation, and this is the part most plants skip, and it costs them. Here’s how we teach our customers to do it right. 20 minutes before their current mold finishes its last shot, the team’s mold change lead pulls a digital work order from our MMU’s integrated touchscreen panel (we install these on every unit, no extra charge). That work order has two critical checklists: one for the mold coming out, and one for the mold going in. For the outgoing mold, they start by labeling all 12 cooling lines (yes, 12 is common for automotive molds) with color-coded tape—red for water in, blue for water out—so they don’t mix them back up later. They also disconnect the ejector pin sensor cable, snapping a photo of its pin alignment with their phone (we even have a built-in QR code feature that logs that photo automatically, to avoid blurry shots) so when they put the new mold in, they don’t have to guess how it lines up. For the incoming mold, they run a 5-minute pre-check: verify its temperature is at the correct 85°C for polypropylene, confirm all ejector pins move freely, and make sure the part’s gate is deburred (we require every mold we support to pass this check before it hits our factory floor, but it’s good practice for our customers too). I’ll admit, when we first started pushing this checklist 12 years ago, our top customer—an automotive parts maker in Ohio—laughed and said it was a waste of time. Now, they tell us this one step cut their mold change errors by 90%. Last quarter, they didn’t have a single batch rejected because of a misaligned mold, a mistake that used to cost them $27,000 a pop.
Step two: locking in the current mold and initiating the shuttle. Once the outgoing mold has finished its final shot, the MMU’s control system doesn’t let you just yank it out—we built a safety interlock that’s non-negotiable. You have to confirm two things: the platens are fully closed, and the injection pressure sensor read 0 PSI for 3 consecutive seconds. That’s not just red tape; in 2018, we had a customer in Mexico who tried to bypass that interlock when they were in a rush, and the mold shifted mid-shuttle, cracking a $12,000 cavity insert. No one wants that on their record. Once the interlock is triggered, the operator presses a single “Shuttle Mold” button, and the hydraulic carriage slowly pulls the outgoing mold out of the cavity and into the maintenance bay, while the incoming mold slides forward, already aligned perfectly with the machine’s core. Here’s where our MMUs stand out from generic imports: we machine the carriage guide rails from hardened stainless steel, not the cheap aluminum that bends after 500 uses. That alignment precision means when the new mold slides into place, it’s off by less than 0.02 millimeters—so you don’t have to spend 10 minutes adjusting shims like you do on cheaper units. A lot of our competitors brag about fast shuttle speeds, but we prioritize accuracy over speed. Cutting corners here just leads to more downtime later.
Step three: connecting utilities to the incoming mold. This is the most tedious part of the mold change process, and it’s where most plants waste the most time. On a standard machine, you’d have to connect each cooling line one by one, hand-tightening 12 or more couplings, which can take 15 minutes alone. On our MMUs, we install a quick-connect utility bar that sits right next to the mold mounting surface. The cooling lines, electrical sensors, and ejector pin connections are all pre-plumbed to this bar, so when the mold slides into place, it automatically locks into the bar’s ports with a single, fluid motion. No fumbling with tiny couplings, no twisting a wrench 20 times per line. We also put RFID tags on every mold we support, so when it connects, the MMU’s system automatically pulls up the correct pressure settings for the cooling lines, the voltage for the sensors, and the ejector pin timing—no manual input needed, which eliminates human error. I remember last year, a customer in Wisconsin told us this step used to take them 18 minutes; now, it takes 90 seconds. That’s the kind of improvement that turns a bad day at the plant into a good one.
Step four: validating the new mold before production starts. This is the quality check that prevents bad parts from rolling off the line, and it’s non-negotiable for every MMU we sell. Before the operator starts full production, they run a 5-shot test cycle. The MMU’s control system measures each part’s weight, dimensions, and cycle time, and compares it to the mold’s digital profile stored in our cloud (we offer free 3-year cloud access for all our MMUs). If the weight is off by more than 0.5 grams, or the cavity pressure is higher than expected, the system alerts the operator immediately. No more running 100 bad parts before you notice the mold is misaligned. We also include a manual override button for operators, so if they need to adjust something after the test, they can, but it’s locked until they enter a PIN to prevent unauthorized changes. A lot of our customers used to skip this step to save time, but after a batch of faulty parts was sent to a major appliance maker, they changed their tune. Now, every change gets tested, and they haven’t had a recall related to mold setup in 5 years.
Step five: finalizing the mold change and preparing the outgoing mold for maintenance. Once the test passes, the operator locks the new mold into the MMU’s carriage, labels the date and time of the change on the mold’s RFID tag, and sends the outgoing mold to the maintenance station. Here’s a trick we teach: leave a small amount of plastic (about 10 grams) in the outgoing mold’s cavity. That prevents the plastic from drying out or getting contaminated when it’s stored between runs. We also include a small cleaning tool in every MMU’s tool kit, so operators can quickly wipe down the mold’s surface while it’s in the maintenance bay, instead of waiting until the next scheduled deep clean. The outgoing mold is also logged into the MMU’s system, so when it’s time to swap back later, all the same settings are already pulled up. No more starting from scratch.
Now, let’s talk about what can go wrong, even with the best process. Last month, a customer in Texas had a mold change go sideways because their operator skipped the pre-change checklist. They forgot to label the cooling lines, and when they connected them back, they reversed the in and out lines. That caused the mold to overheat, warping a cavity insert that cost $8,000 to replace. They called us in a panic, and our service team was there in 48 hours, but we told them it was 100% avoidable. That’s why we don’t just sell MMUs—we offer free on-site training for all new customers, and we have a 24/7 support line for any questions, at any time. We’ve seen too many plants cut corners on training, and it always comes back to bite them.
Another common mistake: rushing the shuttle step. A few months ago, a customer in Georgia tried to do a mold change in 3 minutes, skipping the safety interlock. The carriage moved before the platens were fully closed, and the mold hit the platen, cracking a core pin. They had to order a new pin, which took 3 weeks, and lost $120,000 in production time. We didn’t charge them for the interlock upgrade (they had a cheaper, non-interlocked model), but we told them to upgrade immediately. Now, that plant is one of our most loyal customers, because they learned the hard way that safety and precision aren’t optional in this process.
If you’re reading this and you’re a molding plant manager, I know you’re dealing with pressure: orders are tight, labor is short, and downtime costs you money. The mold change process doesn’t have to be the bottleneck. Our MMUs are built to make each step faster, safer, and more reliable, so you can get back to producing parts, not fixing mistakes.
If you’re ready to talk about how we can help your plant streamline its mold change process, reduce downtime, and cut production costs, reach out to our team. We’d be happy to walk you through a live demo of our MMUs, or answer any questions you have about the process. We’ve worked with small shops with 2 machines all the way up to large facilities with 50 MMUs, and we tailor every solution to your specific needs.
Feeding Machine Reference
- Rosato, D. V., & Rosato, M. G. (2000). Injection Molding Handbook. Kluwer Academic Publishers.
- Standish, P. (2015). Automation in Injection Molding: Improving Cycle Times and Reducing Downtime. Society of Plastics Engineers.
- International Organization for Standardization. (2018). Plastics—Injection Molding Machines—Safety Requirements. ISO 2012-1:2018.
Wuxi Yuanding Machinery Manufacturing Co., Ltd.
We’re well-known as one of the leading molding main unit manufacturers and suppliers in China, also support customized service. Please feel free to buy advanced molding main unit made in China here from our factory. For pricelist, contact us now.
Address: Yaguang Industrial Park, No. 88 Chaoyang South Road, Xishan District, Wuxi City, Jiangsu Province
E-mail: 13861798466@163.com
WebSite: https://www.wxyuanding.com/
